Engineered Extension Cord Reels & Power Distribution Outlets
Manufactured from virgin flame-retardant polymers, high-conductivity phosphor bronze conductor tracks, and heavy-gauge pure copper cables to eliminate heat buildup and meet stringent global electrical standards.
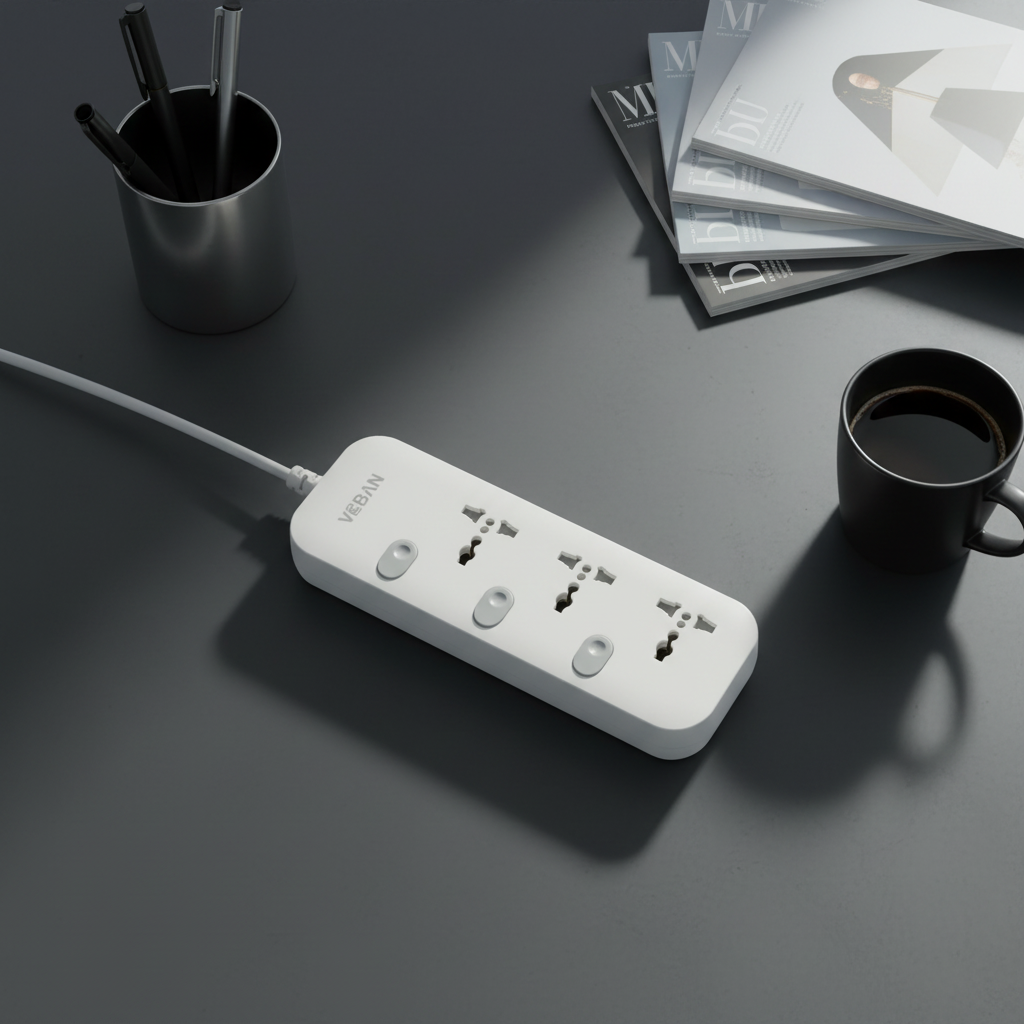
Hot Sale Universal Power Strip 3 Outlets Separate Switch Extension Cable Socket with Children Security Overload protection
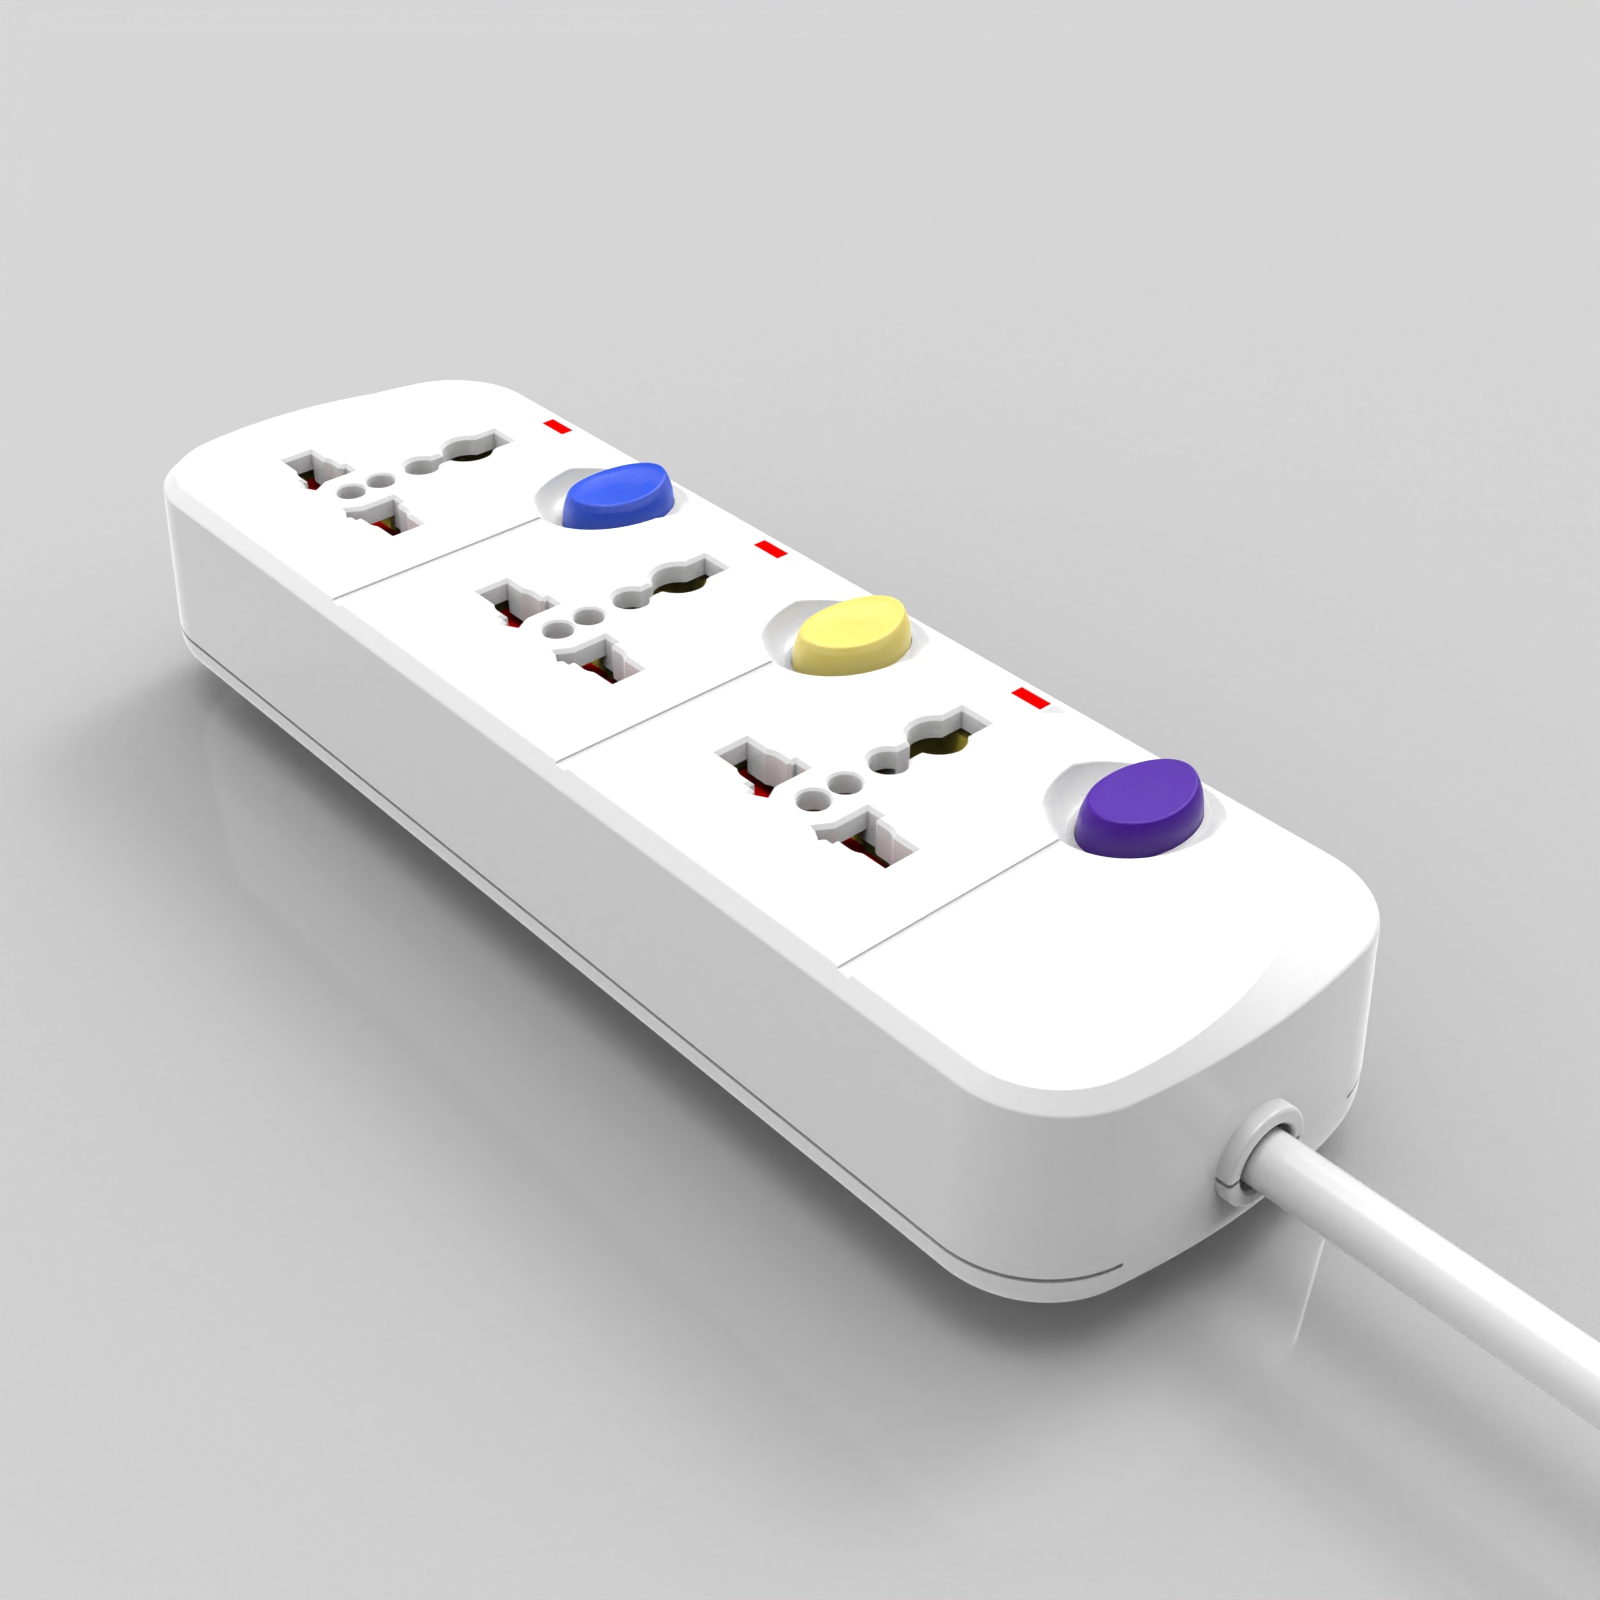
Basic 3 Way Universal Power Strip Extension Socket with Colorful Separated Switches
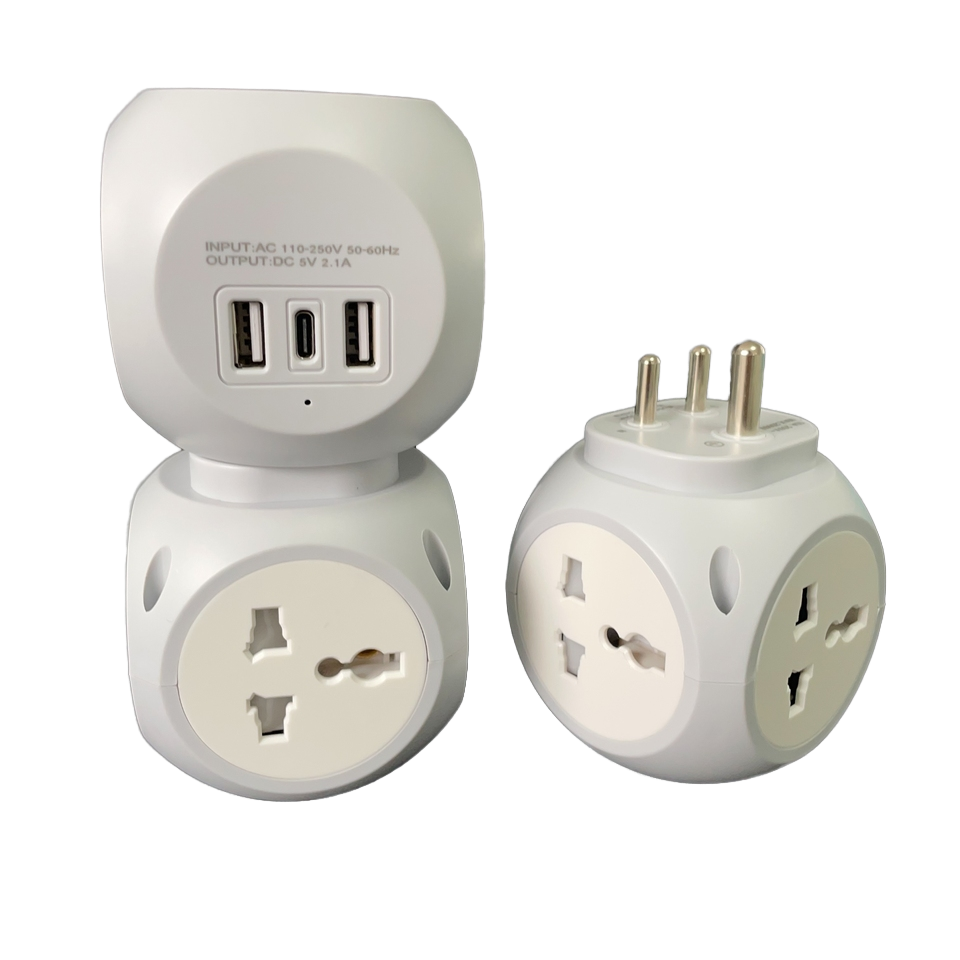
10A Cube Adapter 3 Round Pin South Africa Plug Travel Adapter Mini Size 4 Way Universal Socket Power Strips with USB and Type C
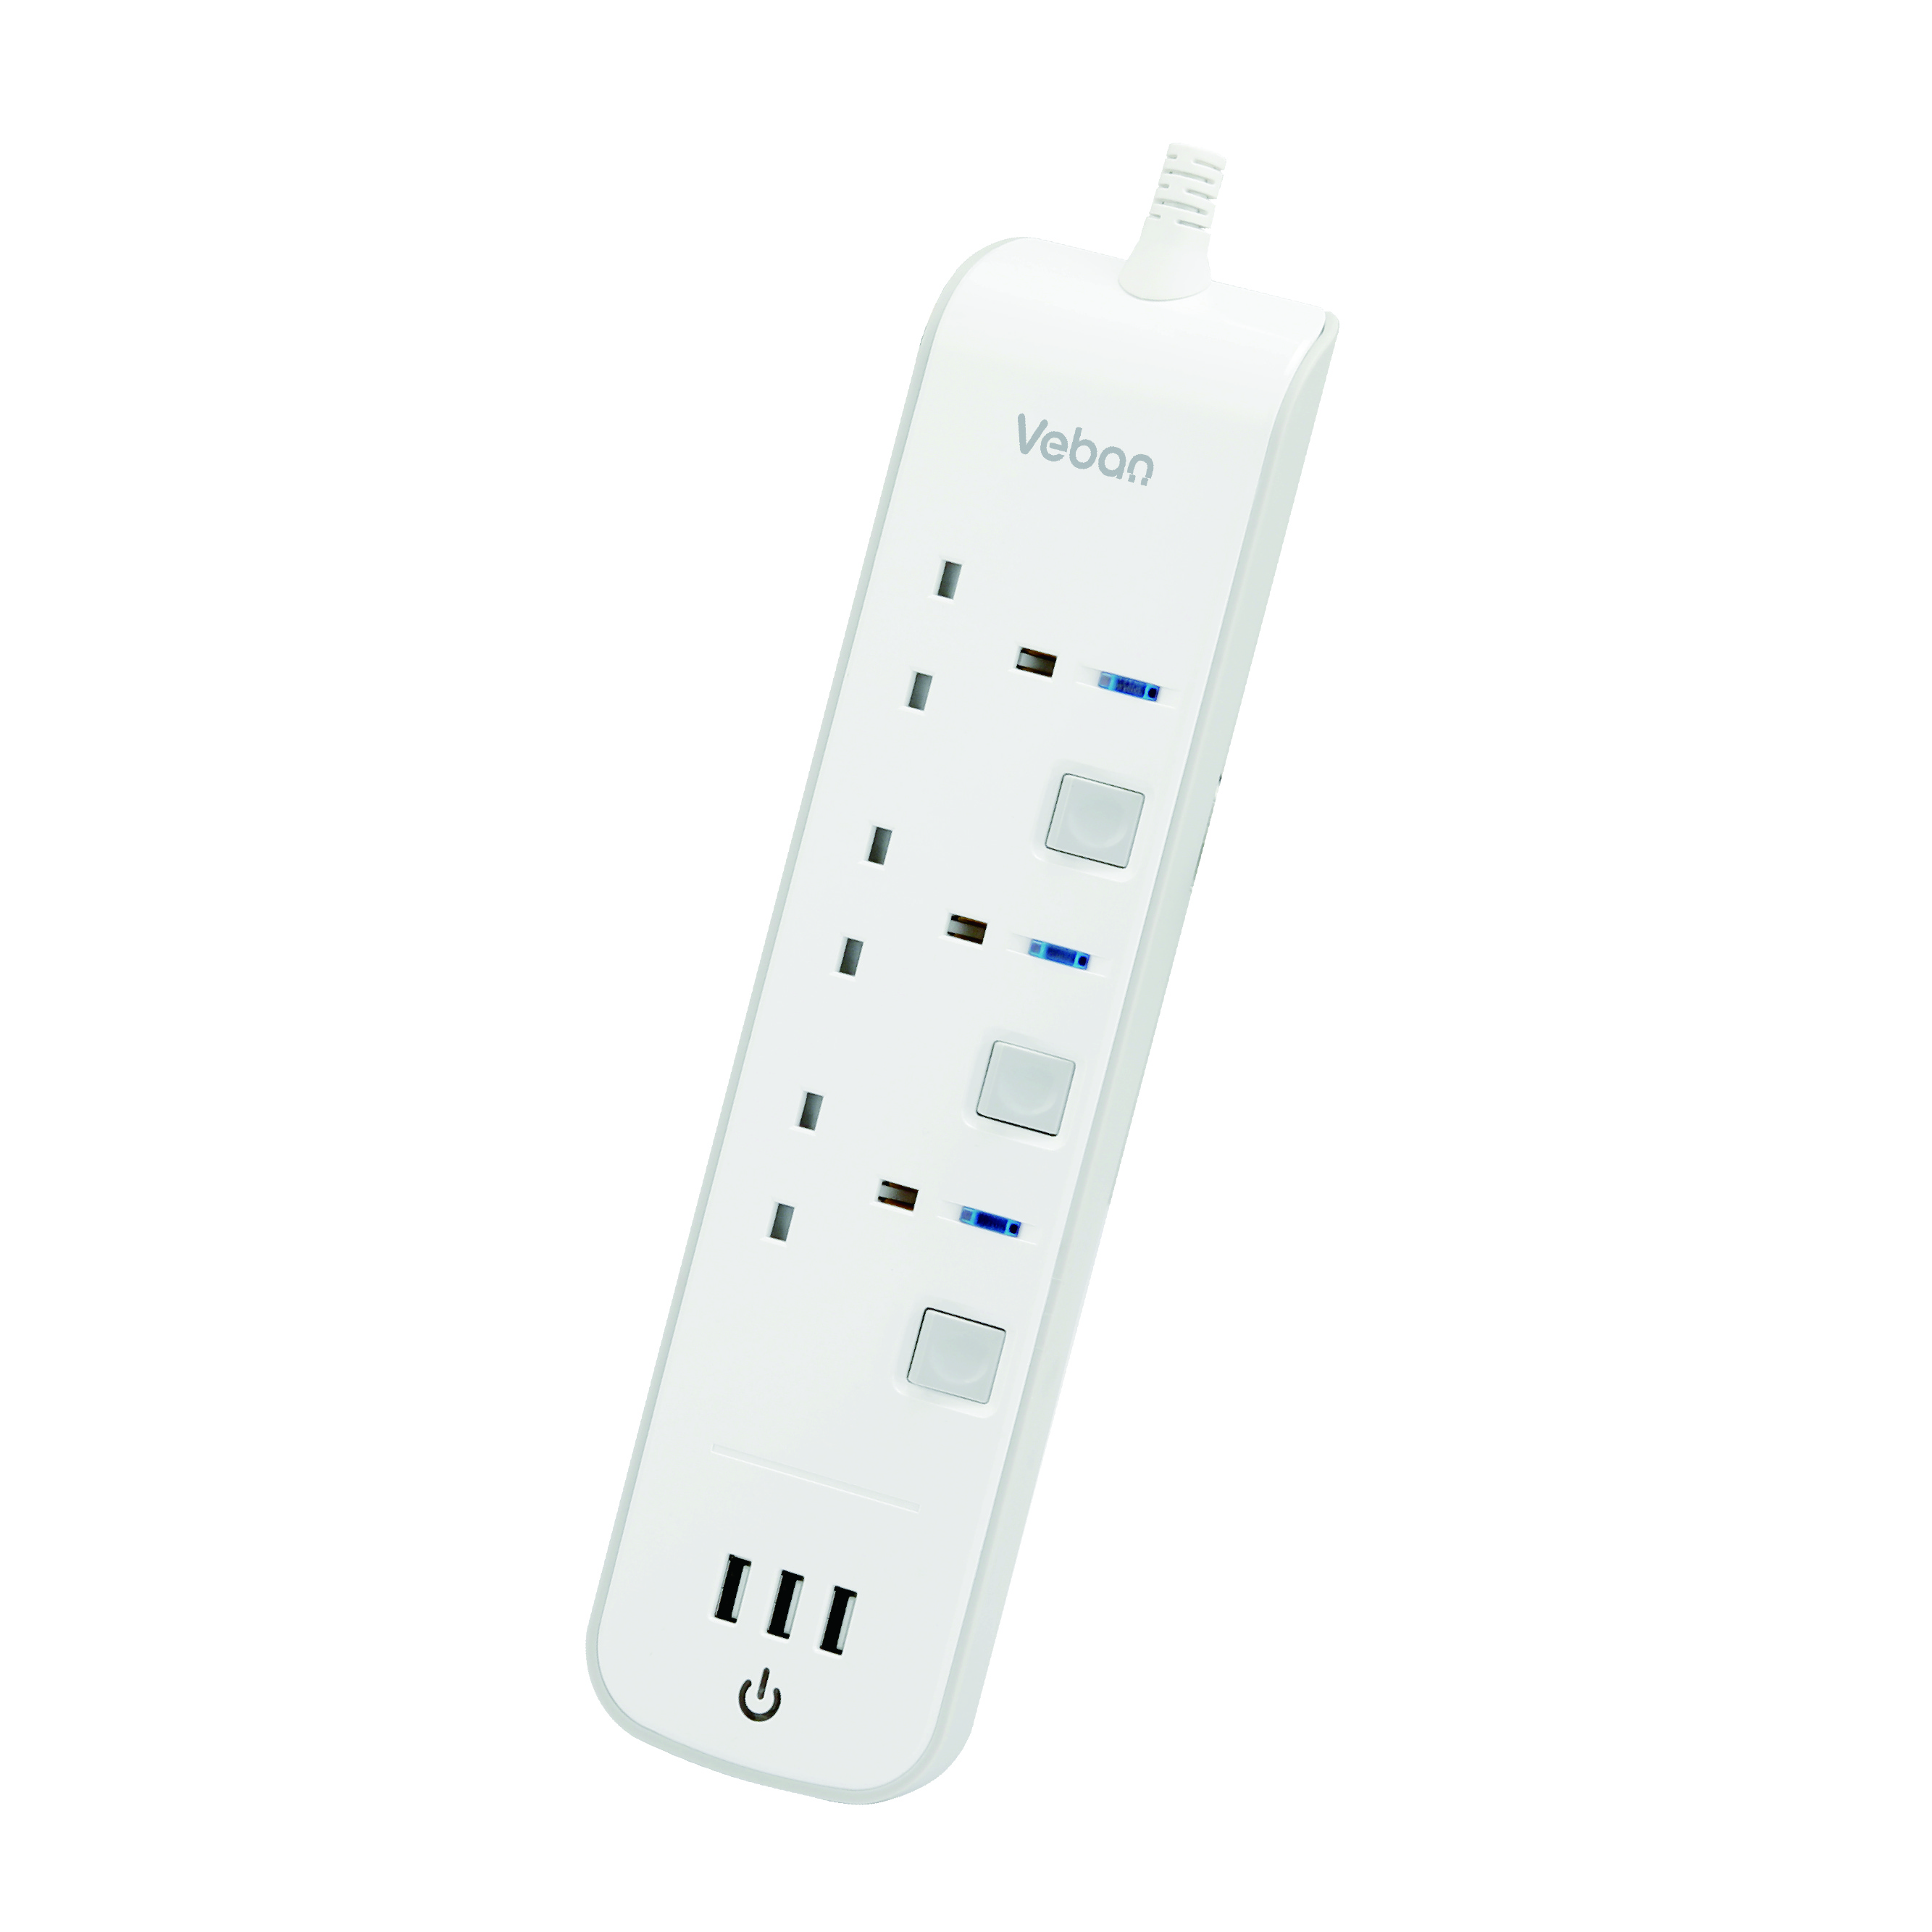
VEBAN Basics Smart Plug Power Strip with 3 Individually Controlled Outlets and 3 USB Ports UK Power Strip with Children Security
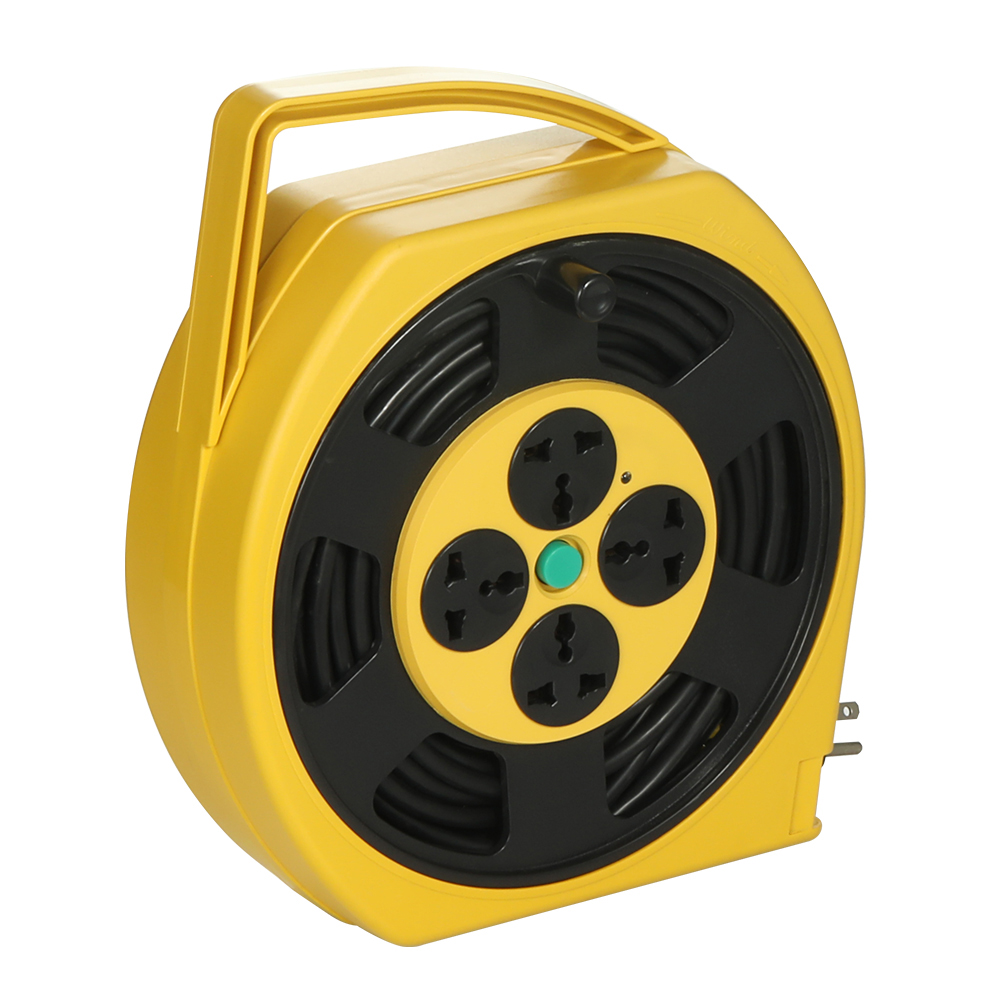
Mini Cable Reel with Wind Handle Retractable Extension Cord Power Indicator 10-20 M Suitable for Home and Inside Use
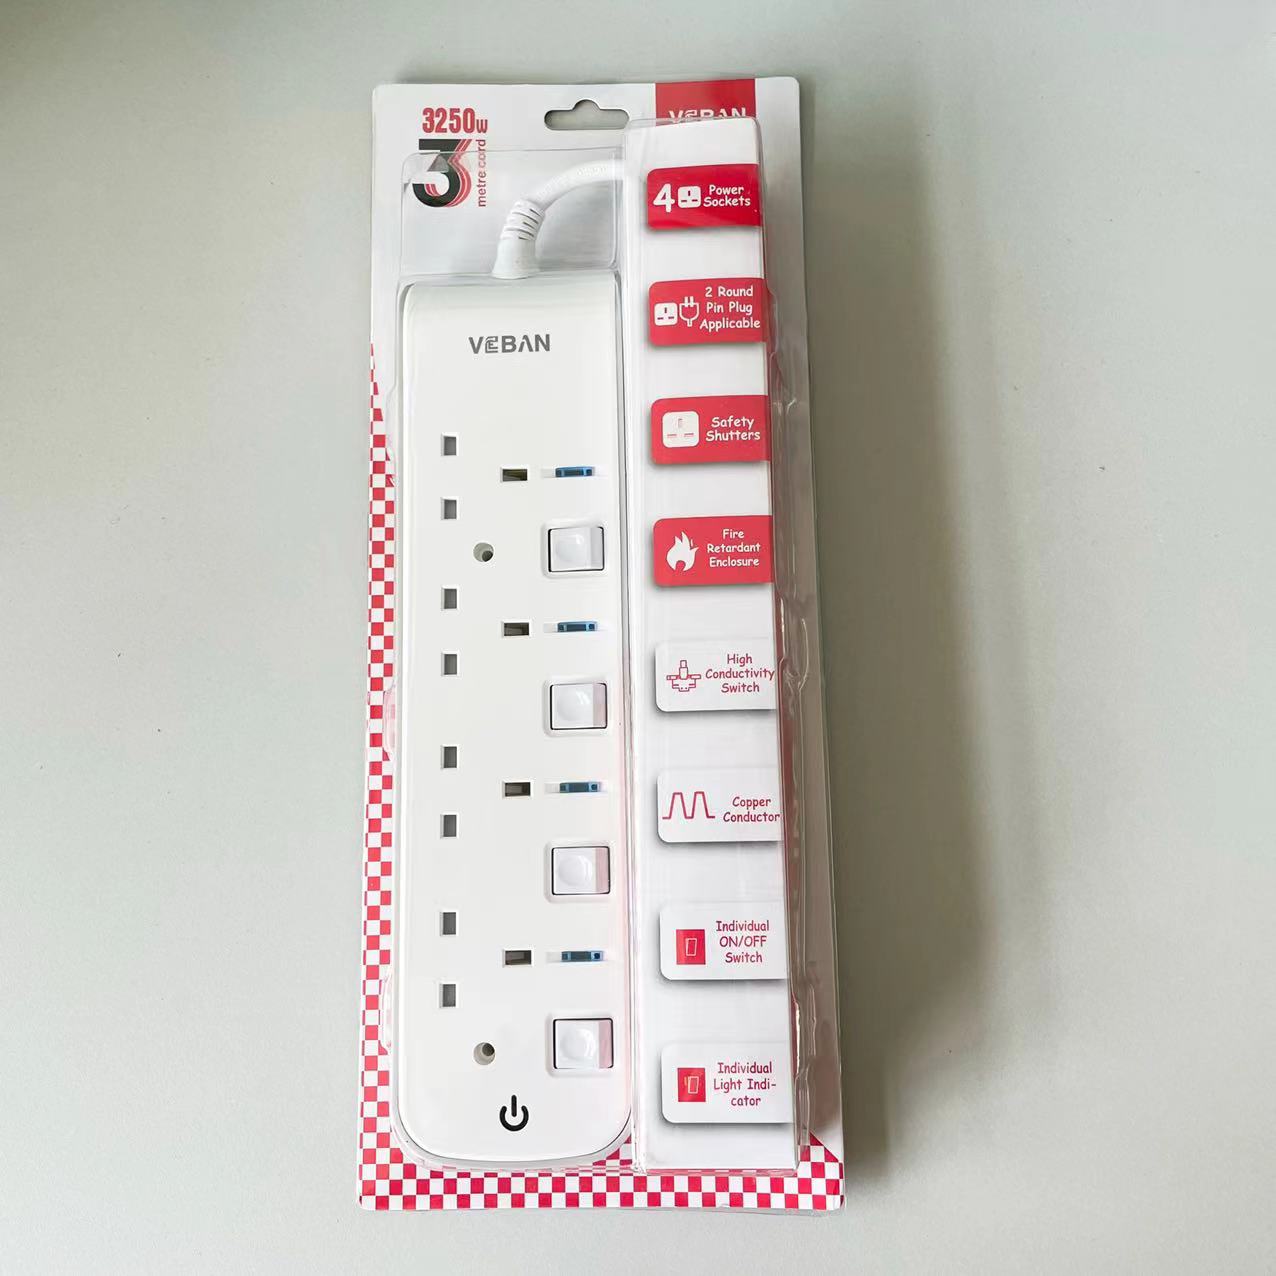
Multiple Power Socket Strip High Quality IEC Standard 13A Multi Plug Socket with 2M 3M Extension Cord for Computer TV
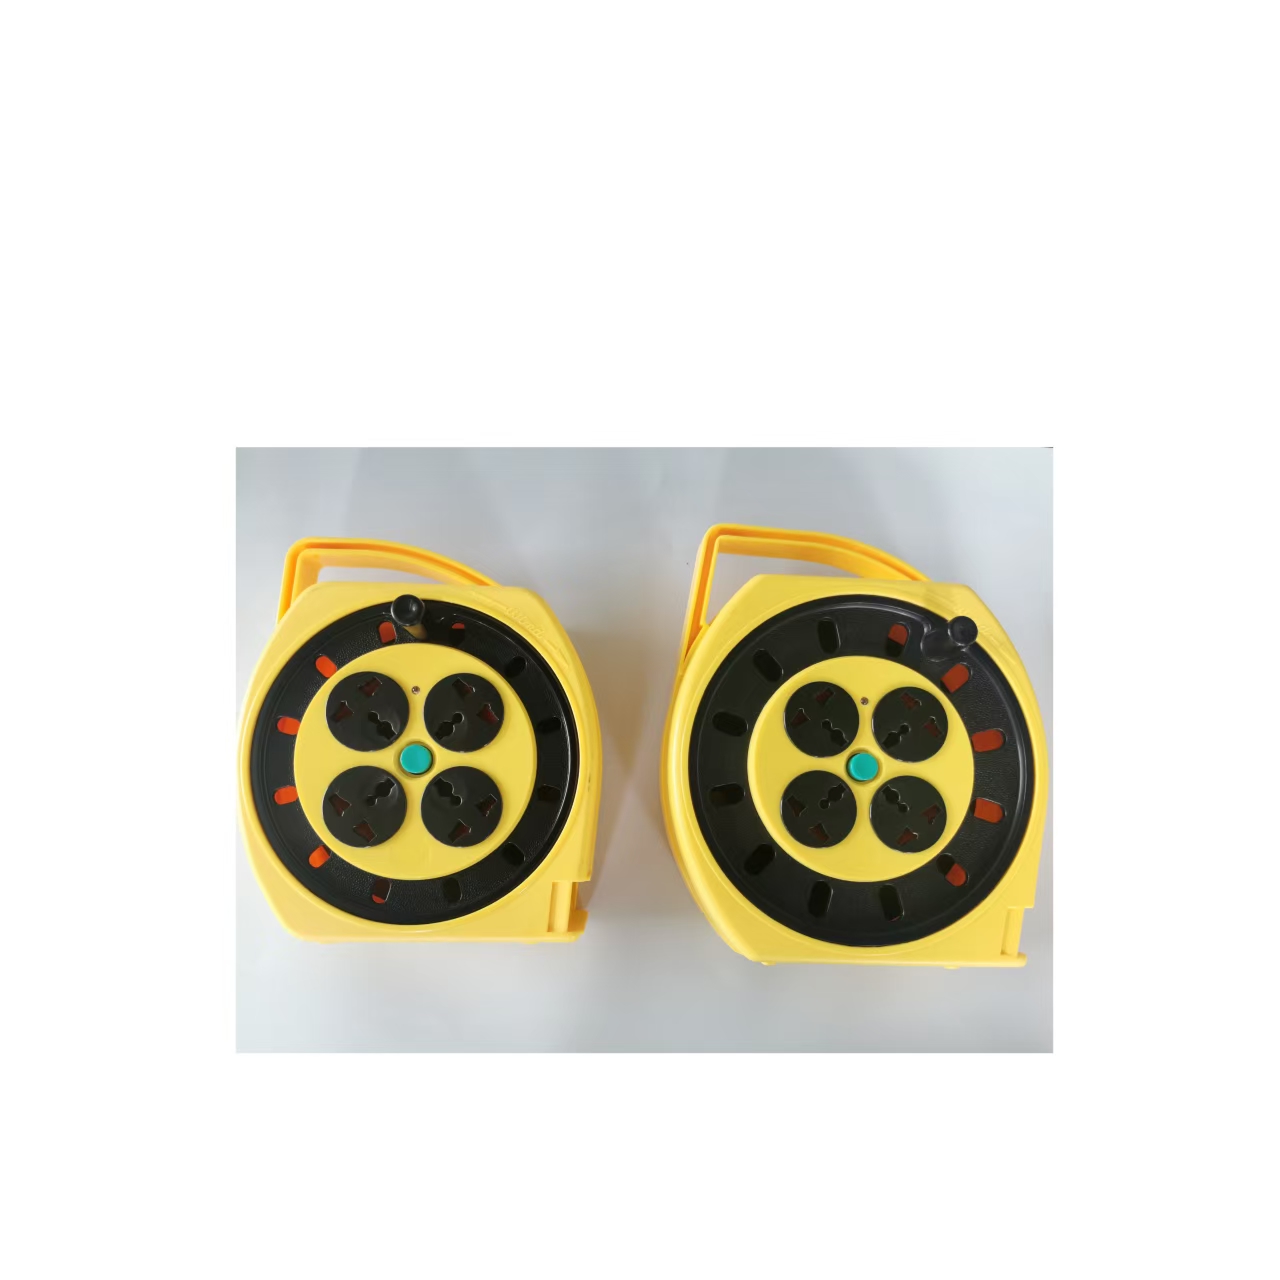
Electronic Extension Cable Reel Power Socket Master ON/OFF Switch Customized Plug EU/UK/US
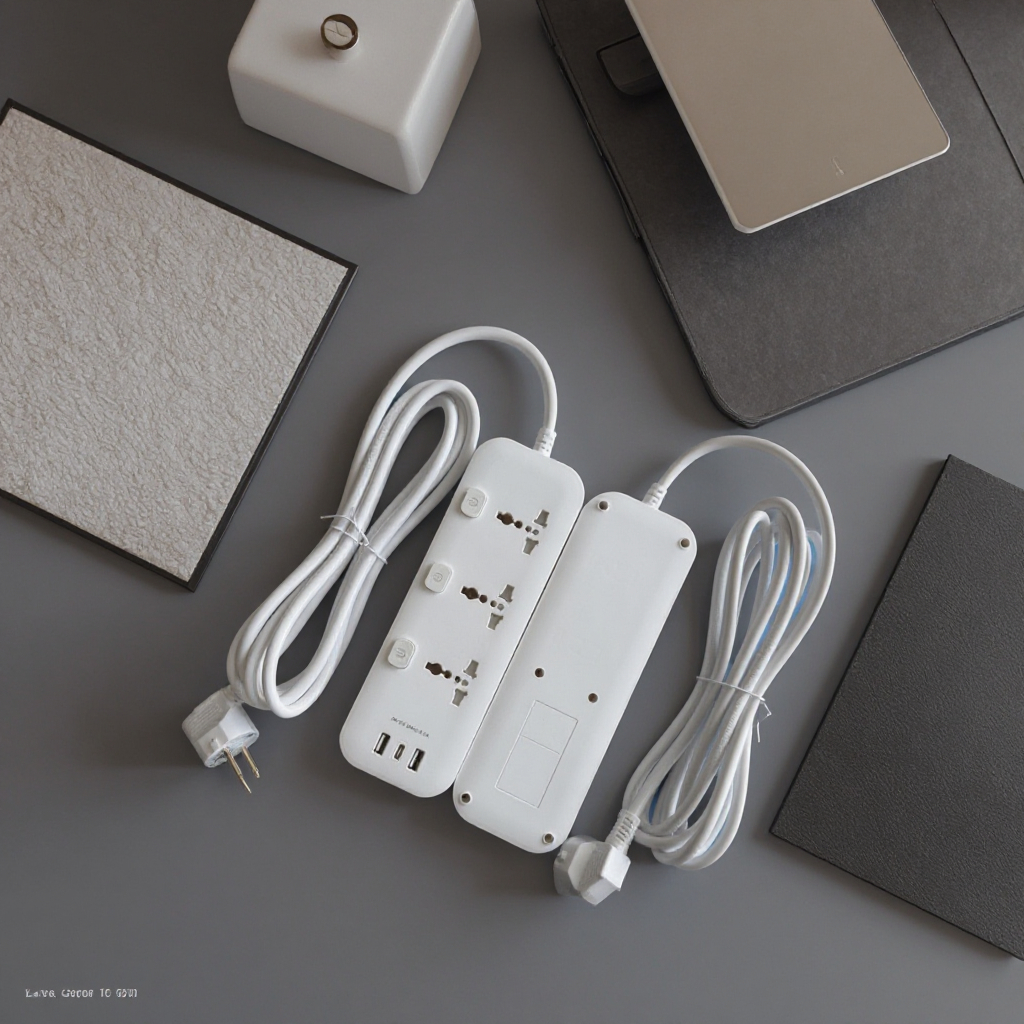
CE Certified 3Way Universal Extension Socket with USB and Type C Charging Output Individual Switches Indication Light
The Global Strategic Shift in Extension Cord Reel Sourcing
As electrical safety norms tighten under EU Low Voltage Directive (LVD 2014/35/EU), British Standard BS 1363, and GCC Standardization Organization (GSO) safety technical regulations, international brand owners and procurement directors face unprecedented scrutiny. The era of sourcing power distribution hardware from non-verified assembly brokers or trading middlemen has closed. Sourcing engineers require deep structural visibility into raw conductor purity, flammability retardance metrics, Joule-rated surge suppression, and internal mechanical contact architectures.
Modern electrical extension cord reels and modular multi-socket distribution units serve as critical junctions in residential, commercial construction, and harsh industrial environments. A single micro-ohmic contact impedance flaw or sub-gauge conductor line can cause rapid thermal accumulation, leading to insulation breakdown, catastrophic arcing, or severe localized fire hazards. Hence, partnering with an audited, vertically integrated manufacturer capable of executing precision stamping, injection tooling, copper drawing, and full automated dielectric breakdown testing is the cornerstone of sustainable brand protection and liability risk mitigation.
Procurement Intelligence: The Risk of "Wound Thermal Throttling"
A crucial technical nuance frequently overlooked by novice commercial buyers is the distinct disparity between fully unwound power capacity and coiled power capacity on drum cable reels. A tightly wound 50-meter cable functions as a continuous heating coil. If operated at rated current (e.g., 16 Amperes) while coiled, thermal dissipation is trapped within the core layers, elevating internal cable temperature past the 70°C PVC degradation threshold within 25 minutes. High-grade OEM suppliers integrate bi-metallic snap-action thermal overload protectors set strictly to 56°C ± 5°C with manual push-button reset mechanisms, guaranteeing circuit interruption long before the polymer reaches its auto-ignition point.
Comprehensive Engineering Comparison: Industrial vs. Commercial Grade Reels
| Evaluation Parameter | Commercial / Residential Cord Reels | Heavy-Duty Industrial Reel Assemblies | Fenvo High-Specification Advantage |
|---|---|---|---|
| Drum Construction | Recycled ABS / Polystyrene Blend | Heavy-gauge Virgin Polypropylene / Steel Frame | High-impact virgin PP with UV inhibitors & drop-test proof tubular steel |
| Internal Conductor | Segmented Wire Solder / Riveted Brass | Stamped Integrated Phosphor Bronze Busbar | Seamless cold-punched H62 copper alloy with zero-rivet current path |
| Cable Jacket Spec | Standard H05VV-F PVC Sheathing | H07RN-F Neoprene Synthetic Rubber | Customized H05VV-F, H07RN-F or oil-resistant halogen-free formulations |
| Thermal Overload Device | Optional / Single-pole slow blow | Automated Bi-metallic Thermal Switch | Self-resetting or manual trip calibrated precisely to VDE 0620 / BS EN 61242 |
| Ingress Protection | IP20 (Dry Interior Only) | IP44 / IP54 (Sprung Flip Covers) | Precision silicone gasketed lids with drainage channels (IP44/IP54 certified) |
Future Procurement Trends: The Next-Generation Extension Hardware Ecosystem
Technological convergence in power electronics, renewable micro-grids, and consumer device fast-charging protocols is profoundly reshaping product requirements across the power strip and cable reel market. Enterprise buyers formulating their multi-year supply chain roadmap must prepare for the following four disruptive manufacturing trends:
1. GaN III High-Density Fast Charging Modules
The elimination of standalone charging bricks has transformed multi-plug sockets into primary charging hubs. Traditional silicon transformers are rapidly giving way to Gallium Nitride (GaN) surface-mount chipsets. Next-gen extension reels now embed 35W to 100W USB Power Delivery (PD 3.0/3.1) Type-C circuits with Dynamic Power Allocation, keeping PCB temperatures below 55°C within ultra-compact form factors.
2. Halogen-Free Flame Retardant (HFFR) Polymers
Under expanding European RoHS 3, REACH, and circular economy directives, traditional brominated and chlorinated flame-retardant resins are facing phased bans. Global distributors are prioritizing self-extinguishing polycarbonates (UL94 V-0 at 0.75mm) and bio-based Polyamide 66 matrices that produce zero toxic hydrogen halide vapors and achieve glowing wire ignition indices (GWIT) above 850°C.
3. Embedded Telemetry & Micro-Current Safety
Industrial job sites and smart office environments increasingly require real-time load analytics. New reel developments integrate low-power Bluetooth Low Energy (BLE) and Matter-compatible Wi-Fi micro-controllers that monitor line voltage, leakage current, and thermal runaway. These smart sensors automatically trigger digital trip relays before mechanical breakers trip, reducing costly downtime on critical construction equipment.
Strategic Supplier Qualification: Shifting from Price-Per-Meter to Total Cost of Ownership
Modern B2B buyers have abandoned transactional quote-driven procurement in favor of life-cycle durability metrics. Substandard copper clad aluminum (CCA) cables masquerading as oxygen-free copper (OFC) represent an enormous financial and legal trap. CCA conductors demonstrate 40% higher resistance per meter, causing excessive voltage drop, dangerous skin-effect heating under AC loads, and accelerated fatigue fracturing after repeated coiling cycles. Direct factory auditing must mandate spark-emission spectroscopic verification of copper purity (≥ 99.95% Cu) and continuous spark testing of the extruded sheath at 6,000V AC.
Global Regulatory Compliance & Import Clearance Blueprint
Navigating cross-border customs authorities and electrical inspection boards requires absolute alignment between product markings, test reports, and the importer of record documentation. Below is the essential compliance matrix maintained across all Fenvo manufactured export lines:
| Geographic Market | Mandatory Standard / Law | Scope & Technical Mandate | Critical Test Criteria | Fenvo Factory Status |
|---|---|---|---|---|
| United Kingdom | UKCA / Electrical Equipment (Safety) Regs 2016 | BS 1363-1 / BS 1363-2 (Plugs & Socket Outlets), BS EN 61242 (Reels) | BS 1362 ceramic fuse in plug, shuttered live/neutral sockets, 13A load testing | Certified Full Compliance |
| European Union | CE Marking / LVD 2014/35/EU, EMC 2014/30/EU | DIN VDE 0620-1 (German Schuko), NF C 61-314 (French Type E), EN 61242 | Dual lateral earthing spring resistance < 0.05Ω, 16A continuous, glow-wire 750°C | Certified Full Compliance |
| Gulf Cooperation (GCC) | G-Mark Technical Regulation BD-142004-01 | GSO BS 1363-2 / SASO 2203 (Saudi Arabia, UAE, Kuwait, Oman) | Mandatory SASO CoC, GCTS QR tracking on unit packaging, Gulf plug geometry | Certified Full Compliance |
| South Africa | NRCS / LOA (Letter of Authority) | SANS 164-1 (Large 3 round pin 16A) & SANS 164-2 (Compact 16A) | Mechanical endurance (10,000 insertions), contact withdrawal force test | Audited & Compliant |
| International General | IEC 60884-1 / IEC 60884-2-7 | Standard multi-standard cord extension sets and portable socket-outlets | Dielectric withstand 2000V / 1 min, temperature rise limit ≤ 45K at terminals | Certified Full Compliance |
Factory Pedigree: Cixi City Fenvo Technology Co., Ltd.
Headquartered in Daqishan Village, Guanhaiwei Town, Cixi, Ningbo, Zhejiang Province, Fenvo Technology stands at the geographic center of the world's most sophisticated electrical accessories manufacturing cluster. Operating over 4,587 square meters of precision manufacturing space with 54 verified technical staff and 4 high-capacity assembly lines, we provide an uninterrupted, fully traceable supply pipeline direct to the world's most demanding electrical retailers and OEMs.
In-House Tooling & Mold Making
We own and manage our core injection mold fabrication. Custom housings, branded drum faces, and proprietary socket layouts transition from CAD to physical T1 prototype molds within 21 business days.
Integrated Cold Stamping
Unlike competitors relying on purchased stamped leaves, our in-house punch division stamps high-elasticity phosphor bronze strips into continuous contact bars, eliminating rivet joints that cause voltage drop.
Automated Cable Extrusion & Reeling
High-speed planetary stranding and jacket extrusion machinery ensures perfect concentricity of insulation, preventing core drift and internal conductor pinching during automated reel winding.
Onsite Electrical & QC Laboratory
Every batch undergoes rigorous batch testing: insertion withdrawal force, temperature rise under 1.25x load, high-voltage breakdown, drop-impact testing at -15°C, and glow-wire thermal chamber trials.
Why Tier-1 Importers Consolidate with Fenvo: Supply Chain Resilience
With an annual export share of 91% to 100% and an annual manufacturing output value between US$5 million and US$10 million, Fenvo’s operational infrastructure is engineered exclusively for international trade compliance. Located less than 65 kilometers from the deep-water Ningbo-Zhoushan Port, our logistics department provides streamlined FOB dispatch, full palletization optimized for 40HQ container cube utilization, and complete digital documentation packs (Declaration of Conformity, RoHs testing reports, and mill certificates for raw copper).
Frequently Asked Questions: Technical & Commercial Due Diligence
Direct answers prepared by our Senior Engineering Director and International Trade Counsel to assist your procurement committee.
1. What are the standard Minimum Order Quantities (MOQs) across your reel and strip catalog?
2. Why does the power rating drop by more than 60% when an extension reel remains coiled?
3. Which specific independent factory verification and audit credentials does Fenvo possess?
4. What is the difference between stamped copper busbars and conventional wire soldering inside power strips?
5. How do you ensure flammability resistance on socket housings and cable jackets?
6. Can Fenvo support custom OEM / ODM tooling and private label packaging?
7. What conductor sizing is recommended for 10A, 13A, and 16A international extension cords?
8. What surge protection components and Joules ratings are integrated into your power boards?
9. What payment terms, lead times, and dispatch ports apply to volume purchase orders?
10. How does Fenvo manage pre-shipment quality assurance and factory acceptance testing?
Ready to Upgrade Your Power Distribution Supply Chain?
Connect directly with Fenvo's senior engineering department in Cixi, Ningbo. Receive full compliance dossiers, direct factory wholesale pricing, and express prototype samples dispatched via DHL/FedEx within 48 hours.