Verified Electrical Power Strips & Extension Hardware
Direct manufacturer supply for overseas wholesalers, EPC infrastructure contractors, and brand-label distributors. Tested for continuous commercial load duty.
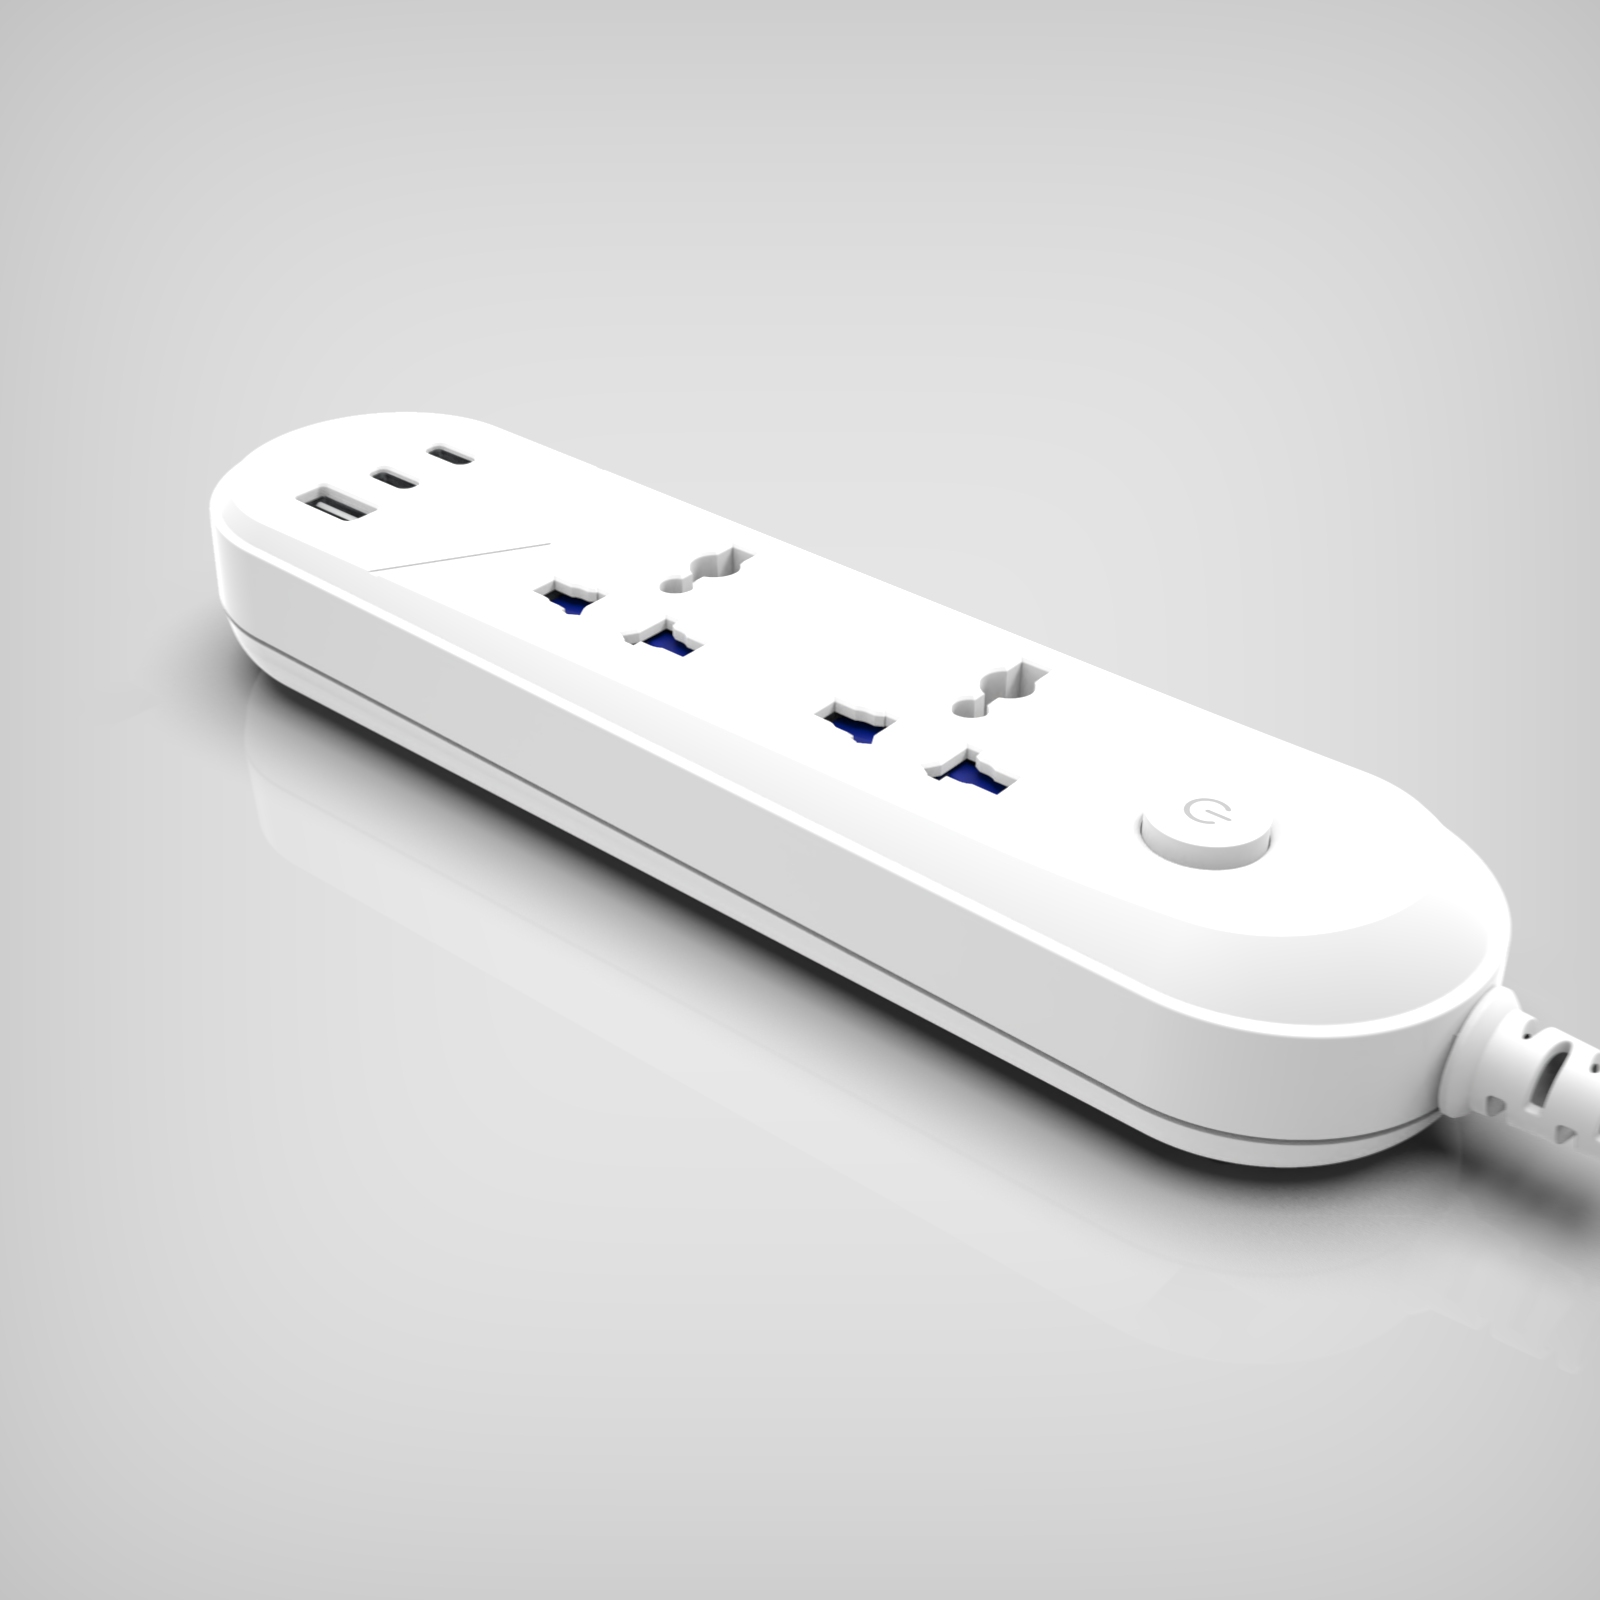
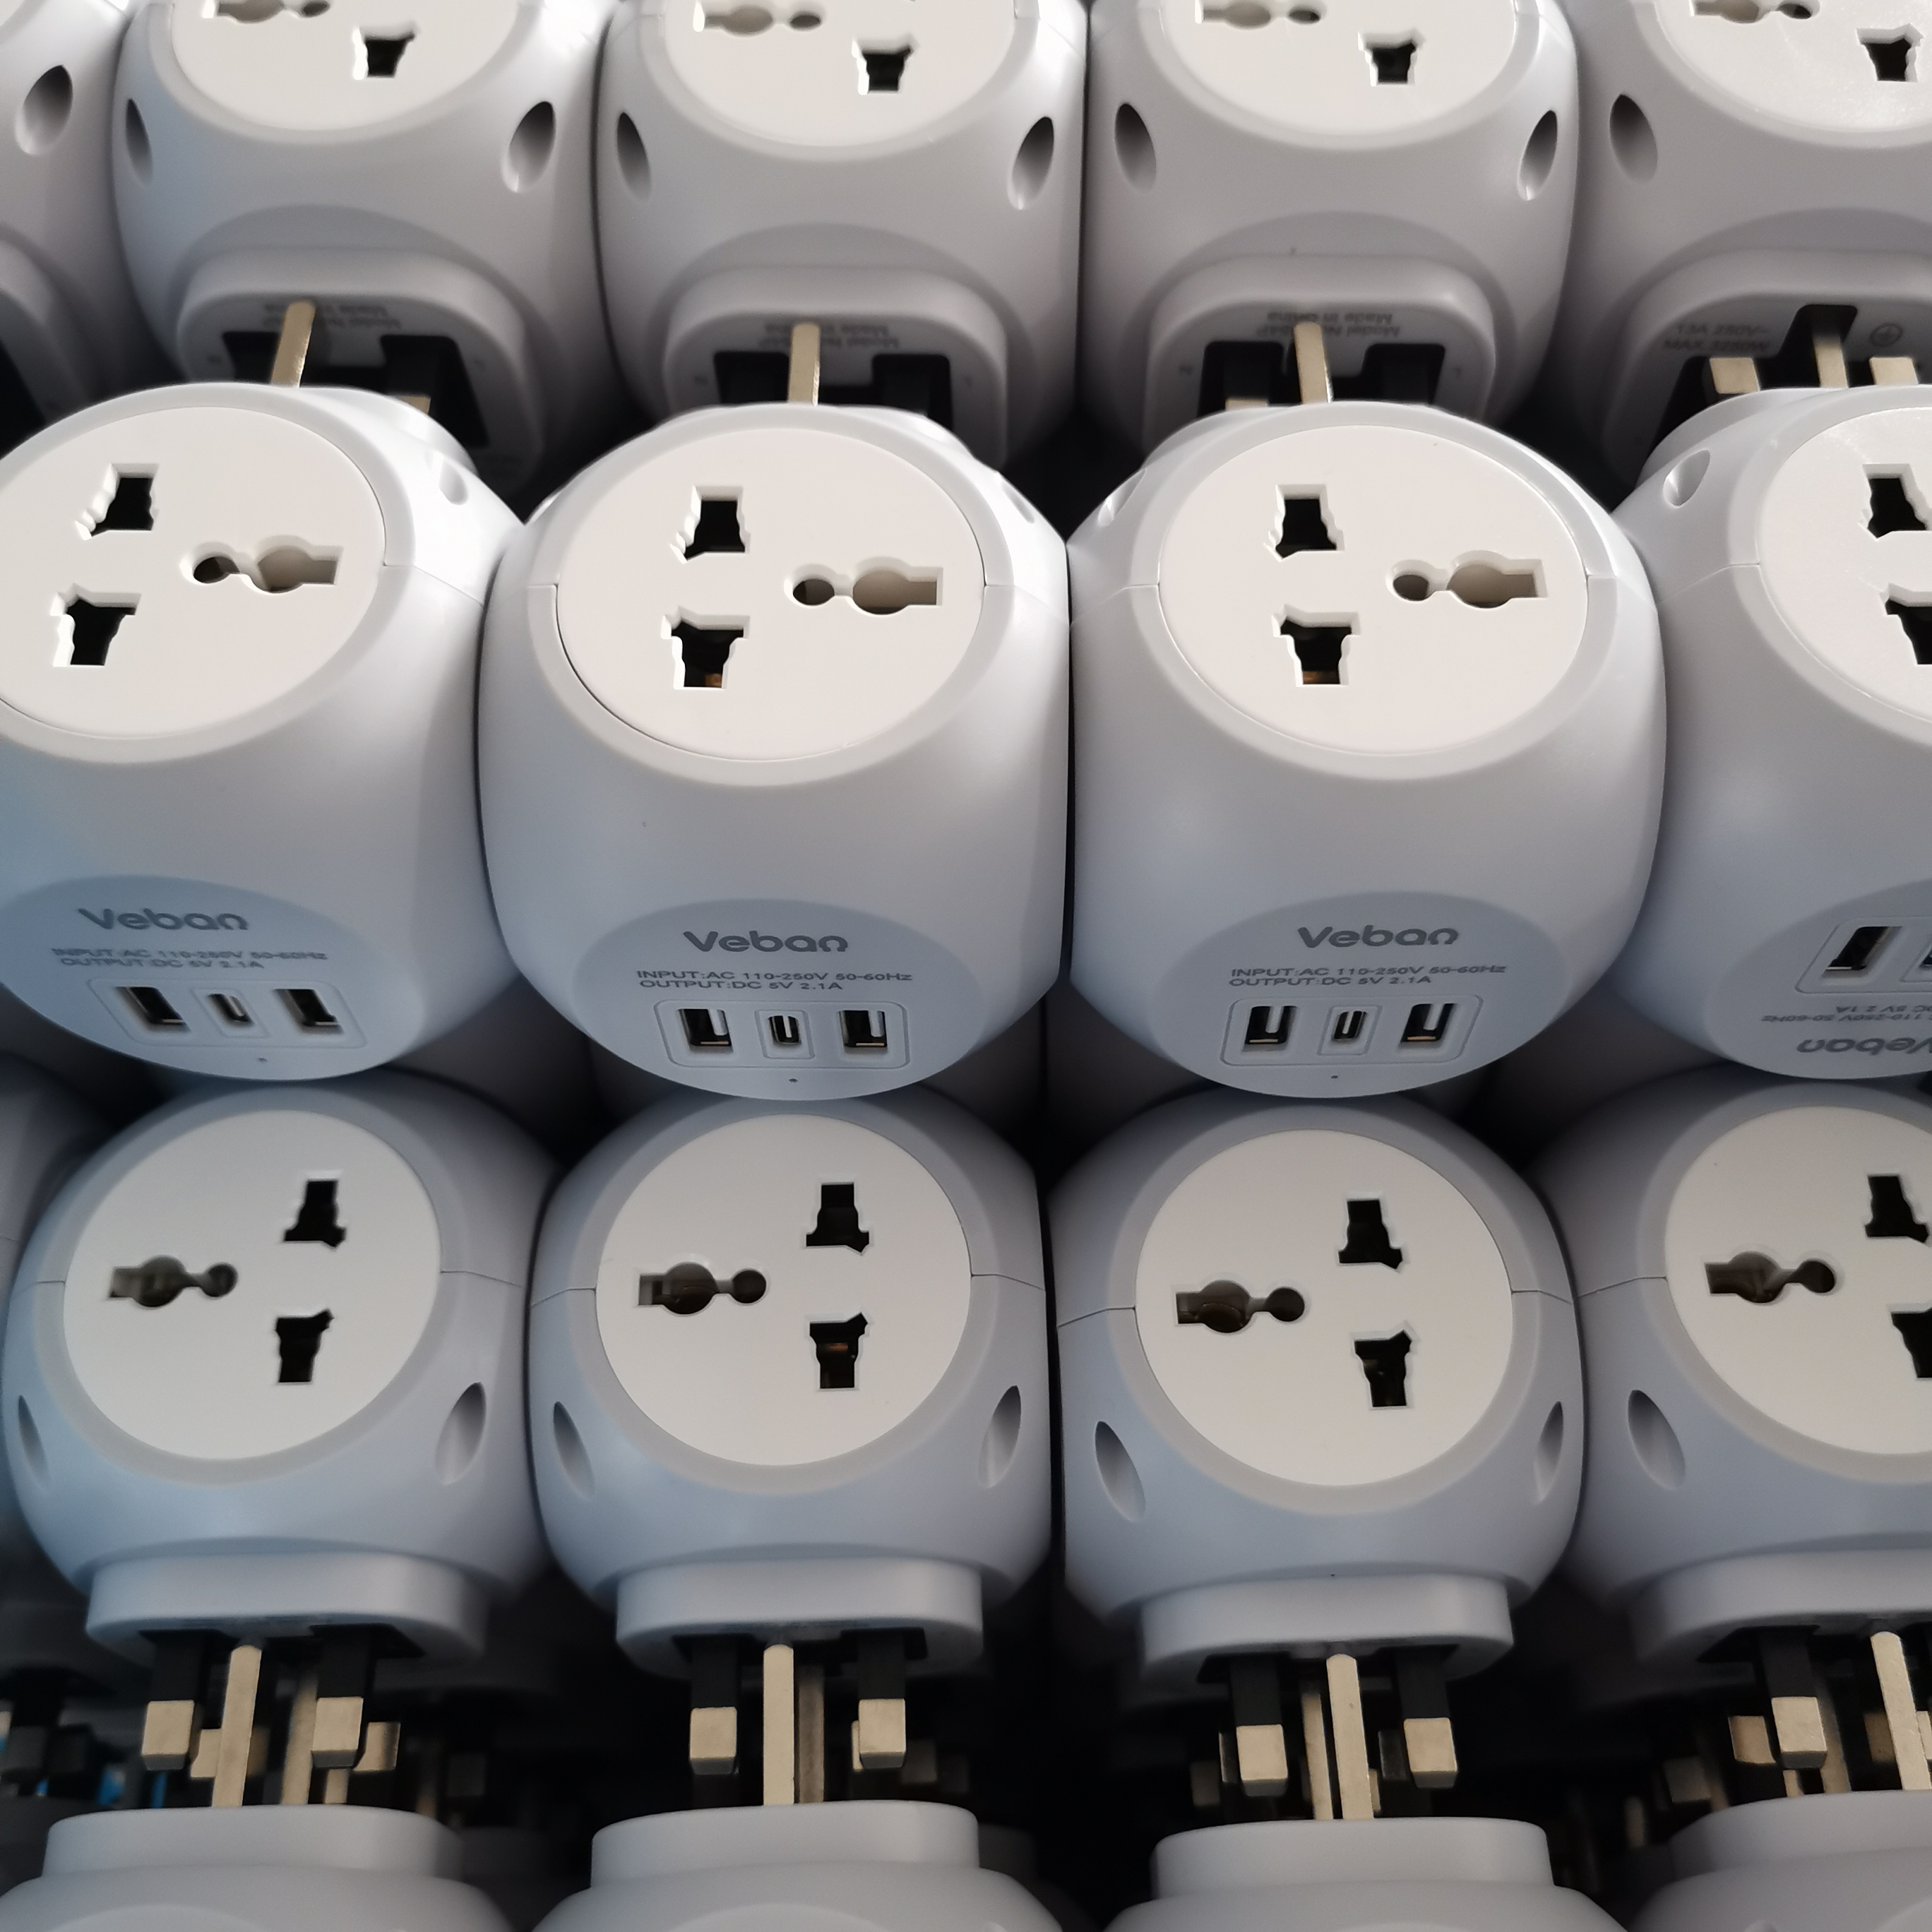
1. Engineering Fundamentals of CE Certified Power Cord Reels
In modern commercial, industrial, and heavy-duty residential environments, power cord reels act as critical electrical links subject to extreme thermal, mechanical, and electrodynamic stresses. For overseas technical procurement teams, a compliance mark on a cord drum is not a cosmetic differentiator—it is a rigorous commitment to international safety protocols governed by the Low Voltage Directive (LVD) 2014/35/EU, the Electromagnetic Compatibility (EMC) Directive 2014/30/EU, and product-specific harmonized standards such as EN 61242 (cable reels for domestic and similar purposes) and EN 61316 (industrial cable reels).
A primary point of thermal vulnerability in tightly coiled extension reels arises from Joulean heating and coil inductance. When high current flows through a tightly spooled cable drum, the internal layers cannot dissipate heat effectively through convection. Under a full 16A European Schuko load or a 13A British Standard load, a coiled reel can experience internal temperature escalation exceeding 95°C within minutes, leading to rapid insulation degradation, dielectric breakdown, and catastrophic melting. CE-compliant manufacturing mandates the integration of non-cycling, bi-metallic thermal cut-out switches calibrated to trip between 56°C and 65°C, requiring manual intervention once the drum cools.
Electrolytic Pure Copper Wire
Conductors manufactured from oxygen-free high-conductivity copper (OFHC ≥99.97% IACS rating) drastically suppress internal line resistance and mitigate voltage drops across extended 20m, 30m, and 50m cable runs.
Flame-Retardant Polymer Drum
Housings injection-molded from UV-stabilized polypropylene (PP) or engineered polycarbonate (PC) meeting the IEC 60695-2-11 Glow Wire Flammability Index (GWFI 850°C/960°C), preventing ignition during arc faults.
Patented Internal Copper Busbars
Replaces hand-soldered fly-wires with monolithic stamped phosphor bronze / brass busbar channels. Eliminates open circuit joint stress, cold welds, and excessive contact resistance under heavy current draws.
2. Technical Comparison: Spooled vs. Unspooled Real-World Ratings
Contractors and commercial electrical distributors must strictly communicate the dual wattage rating inherent to all certified reels. The difference between coiled and uncoiled ratings illustrates why thermal dissipation engineering remains the focal benchmark in export compliance audits.
| Cable Spec & Standard | Conductor Area | Max Load: Fully Coiled | Max Load: Fully Unwound | Thermal Cut-Out Sensor | Compliance Test Status |
|---|---|---|---|---|---|
| H05VV-F 3G1.0mm² (PVC) | 3 × 1.0 mm² | 900W – 1000W (4.3A) | 2300W (10.0A) | 56±5°C Manual Reset | EN 61242 Pass |
| H05VV-F 3G1.5mm² (PVC) | 3 × 1.5 mm² | 1000W – 1200W (5.2A) | 3120W – 3680W (13A/16A) | 56±5°C Manual Reset | CE / UKCA Pass |
| H07RN-F 3G1.5mm² (Rubber) | 3 × 1.5 mm² Heavy Duty | 1200W – 1400W (6.0A) | 3680W (16.0A) | 65±5°C Manual Reset | EN 61316 / IP44 Pass |
| H07RN-F 3G2.5mm² (Site Duty) | 3 × 2.5 mm² Industrial | 1500W – 1800W (7.8A) | 3680W – 4000W (16A+) | Integrated Overload Breaker | Industrial Grade Pass |
3. Future Procurement Trends: Intelligence, Sustainability & Hybridization
B2B buyers sourcing electrical equipment for 2026–2030 are recalibrating their RFQ parameters around four structural trends transforming global power distribution:
1. High-Density GaN (Gallium Nitride) Power Strips & Reels: Modern job sites and creative studios no longer rely solely on AC motors; they demand rapid multi-device field charging. Premium export reels now embed secondary 45W–100W GaN chargers directly into the drum core, reducing PCB thermal footprints and delivering USB-C Power Delivery (PD 3.1) directly from the spool face without requiring bulky third-party AC wall blocks.
2. Micro-Inverter and Battery Storage Interface: The rapid uptake of portable battery power stations has led to an emerging product tier: reversible bi-directional power cord reels designed to interface with off-grid photovoltaic panels and mobile battery banks, fitted with anti-reverse polarity relays and surge protective components (Type 2/3 SPD conforming to IEC 61643-11).
3. Circular Polymer Mandates and REACH/RoHS Traceability: European supply chain directives (such as the EU Corporate Sustainability Due Diligence Directive) place accountability on importers for material composition. Sourcing from manufacturers utilizing certified post-consumer recycled (PCR) engineering polyamides with halogen-free flame retardants is swiftly moving from an optional preference to a statutory purchasing criterion.
4. IP54 Weatherproofing & Heavy Ergonomic Architecture: Standard IP20 open-face drums are losing ground to spring-loaded sealed flap sockets (IP44/IP54). Featuring oil-resistant chlorinated polyethylene or EPR synthetic rubber jacketing (H07RN-F), these units resist UV embrittlement, diesel fluid degradation, and micro-fractures down to -25°C.
Cixi City Fenvo Technology Co., Ltd. — Engineering Superiority
Headquartered in Daqishan Village, Guanhaiwei Town, Cixi, Ningbo — the central cluster of China's electrical socket and cable winding industry — Fenvo Technology integrates 31 years of operational legacy. By internalizing precision copper stamping, thermoplastic injection molding, automatic drum assembly, and automated cable extruding, we preserve complete control over bill-of-materials integrity, eliminate intermediate trade markup, and assure complete batch traceability.
In-House Stamping & Tooling
3 awarded utility patents, high-speed stamping presses, and self-maintained injection tooling ensure dimensional tolerance under 0.02mm for seamless plug-in torque retention.
TÜV Rheinland Onsite Verified
Production facilities, employee headcounts, and clean assembly lines verified through rigorous third-party auditing, ensuring documented supplier reliability.
Full Compliance Documentation
Every commercial production run ships with genuine Declaration of Conformity (DoC), full LVD/EMC test certificates, UKCA paperwork, and GCC registration dossiers.
Agile OEM/ODM Prototyping
Custom cable lengths (5m to 50m), custom socket core inserts (Schuko, French, UK BS, Universal), corporate branding pad printing, and full color box packaging support.
Frequently Asked Questions for Sourcing Directors
Direct technical answers addressing customs clearance, quality control thresholds, and commercial terms.
What are the critical testing criteria for power cord reels to clear CE and UKCA border inspections?
Why do spooled cable reels require a thermal cut-out while short extension sockets do not?
Can Fenvo customize plug types, drum colors, and cord specifications on OEM orders?
What is the standard Minimum Order Quantity (MOQ) and lead time for export shipments?
How does internal copper busbar construction differ from traditional hand-soldered wiring?
What payment methods and trade terms are supported for international accounts?
Ready to Secure Factory-Direct Pricing for Your Market?
Consult directly with our electrical engineering and export compliance specialists. Receive custom quotations, bill-of-materials audits, and compliant physical prototypes within 24 hours.